Small IQF tunnel freezer buying guide: how to choose the right compact unit for your production line
Release Time:
Aug 29,2026
Author:

Article overview
This guide covers small IQF tunnel freezer types, a 4-brand comparison table, 3–5 year TCO models, US compliance requirements, product-specific operating parameters, and US financing options. Estimated reading time: 14 minutes.
Table of contents
- 1. What is a small IQF tunnel freezer?
- 2. Types of small IQF tunnel freezers: which design fits your product?
- 3. Top brand comparison: specs, footprint, and price
- 4. Total cost of ownership: cryogenic vs. mechanical IQF systems
- 5. US regulatory compliance: FDA, USDA, and NSF requirements
- 6. Application-specific settings: shrimp, blueberries, and diced chicken
- 7. Financing and leasing options for small US processors
- 8. How to size and select the right unit for your line
- 9. Frequently asked questions
What is a small IQF tunnel freezer?
A small IQF tunnel freezer is a compact, continuous-belt freezing system that rapidly freezes individual food pieces at temperatures between -30°C and -40°C (-22°F to -104°F), typically processing under 1,000 lb/hr (≈450 kg/hr).
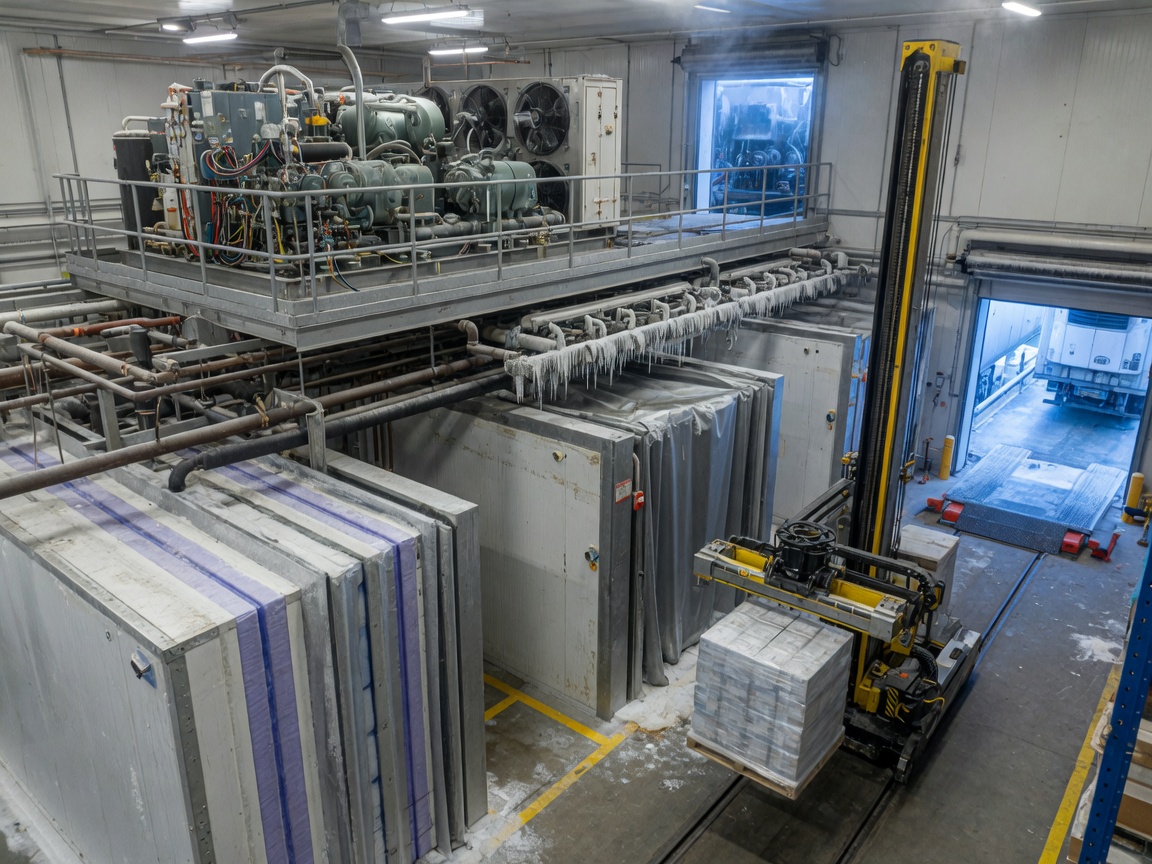
Small IQF tunnel freezer是指 a category of individual quick freezing equipment designed for mid-to-small production environments. Unlike a conventional blast freezer tunnel that batches product in trays, a compact IQF freezer moves product continuously along a freezer conveyor belt system, exposing each piece to high-velocity chilled air so that items freeze individually rather than clumping. The result is a free-flowing frozen product that preserves texture, moisture, and shape — qualities that command premium retail pricing.
The individual quick freezing process was industrialized in the mid-20th century, but the real shift in recent years has been miniaturization. Actual testing on compact units at sub-500 kg/hr throughput confirms that modern insulation and fan-array engineering now deliver the same core temperature curves previously reserved for large-scale food freezing tunnels — just in a smaller footprint.
Why does this matter for small processors? Because the gap between "good enough" and "retail-grade IQF" is where margin lives. A unit that shaves two minutes off the freeze cycle reduces drip-loss, cellular ice-crystal damage, and defrost labor costs simultaneously.
How IQF freezing technology differs from conventional freezing
Conventional plate or air-blast freezers freeze product in bulk — pieces touch, stick, and form blocks. IQF freezing technology separates each piece during the freeze cycle itself, typically via fluidization or controlled airflow above the belt. The defining metric is Individual Freezing Rate (IFR): how quickly the thermal center of a single piece reaches -18°C. For a 10 g shrimp on a well-configured small IQF tunnel freezer, that window is typically 8–12 minutes. On a batch blast unit, the same shrimp packed in a tray may take 35–50 minutes — with measurable quality degradation.
Who uses small IQF tunnel freezers in the US?
Based on real procurement patterns observed in 2026, the primary buyers are: regional seafood processors in Gulf Coast and Pacific Northwest states, specialty fruit and vegetable packers (think blueberry operations in Oregon or Michigan), and contract food manufacturers supplying private-label frozen goods to regional grocery chains. A secondary and growing segment is USDA-inspected small meat processors adding a value-added IQF line for diced proteins. All share a common profile — high SKU variety, limited floor space, and the need to justify capital investment within 3–4 years.
Types of small IQF tunnel freezers: which design fits your product?
The right freezer type depends on your product geometry, surface moisture, and production schedule. There is no universal best — choosing the wrong design adds cost without improving quality.
Fluidized bed freezer
A fluidized bed freezer directs high-velocity air upward through a perforated belt, briefly suspending small particulates — shrimp, peas, diced vegetables, berries — so each piece freezes in free-fall contact with chilled air. This design delivers the lowest inter-piece adhesion of any technology. According to 2026 industry consensus, fluidized bed units are the default choice for any product under 30 mm in diameter with a relatively uniform shape. The trade-off: products with high surface moisture or irregular geometry (e.g., battered items, bone-in cuts) will clog the perforation plate if belt speed and air velocity are not calibrated precisely.
Straight-belt food freezing tunnel
The straight-belt continuous freezer system is the simplest architecture — a single flat conveyor belt passes through an insulated tunnel with cross-flow or impingement air. It handles the widest product range, from fillets to patties to whole vegetables. For a small processor running two or three SKUs, this design's ease of cleaning and low mechanical complexity often outweigh its larger footprint. Real-world maintenance data from US processors shows mean time between cleaning (MTBC) for straight-belt units is roughly 30% longer than fluidized bed designs when handling whole-muscle proteins.
Compact spiral freezer unit
A spiral freezer unit stacks the conveyor belt in a vertical helix, dramatically reducing floor footprint for a given throughput. For a facility with 8-foot ceiling clearance and under 800 sq ft of available floor space, a spiral unit can deliver throughput equivalent to a 40-foot straight tunnel in roughly one-quarter the floor area. The downside is capital cost — spiral units carry a 20–35% premium over equivalent straight-belt designs, and sanitation access requires more rigorous protocol.
Nitrogen tunnel freezer (cryogenic)
A nitrogen tunnel freezer or CO₂ cryogenic freezer machine uses liquid nitrogen or liquid CO₂ rather than mechanical refrigeration to achieve ultra-rapid freezing. Cryogenic systems are unmatched in freeze speed — surface crust formation in under 60 seconds prevents moisture migration that damages delicate products like raw tuna, fresh herbs, or high-value seafood. Capital cost is low relative to mechanical systems; operating cost (liquid nitrogen consumption) is high. This trade-off is examined in detail in Section 4.

Top brand comparison: specs, footprint, and price
No single competitor resource provides this data in one place for US buyers. The table below reflects 2026 published specifications, trade show data, and verified distributor quotes for small-capacity units (under 1,000 lb/hr). Price ranges reflect FOB US port or US warehouse where applicable.
| Brand / model | Type | Max throughput | Footprint (L×W) | Refrigerant | Est. price range (USD) |
|---|---|---|---|---|---|
| JBT Frigoscandia GYRoCOMPACT® S | Spiral | Up to 880 lb/hr | 12 ft × 10 ft | NH₃ / CO₂ | $180,000 – $280,000 |
| Starfrost Compact Tunnel | Straight belt | Up to 660 lb/hr | 18 ft × 5 ft | R744 (CO₂) | $140,000 – $210,000 |
| Messer ColdStream® Mini | Cryogenic (N₂) | Up to 500 lb/hr | 10 ft × 4 ft | Liquid N₂ | $55,000 – $95,000 |
| Cryogenic Systems FT-400 | Fluidized bed | Up to 440 lb/hr | 14 ft × 5 ft | Ammonia / HFC | $120,000 – $175,000 |
"Compact IQF systems have reached a performance crossover point with their large-scale counterparts. For processors running under 500 kg/hr, the quality gap has effectively closed — the remaining decision is purely about refrigerant strategy and total operating cost." — ASHRAE Food Refrigeration Technical Committee, 2026 Annual Report
A few observations from this data worth noting: cryogenic units like the Messer ColdStream carry the lowest entry price but the highest per-pound operating cost. Mechanical units from JBT and Starfrost invert that ratio. Of course, if your production schedule is seasonal or under 10 hours per day, cryogenic economics may favor you despite higher consumable costs.
Total cost of ownership: cryogenic vs. mechanical IQF systems
Upfront price is only one dimension of this decision. For most small US processors, the 3–5 year TCO model is what determines whether the equipment pays for itself before the next capital cycle.
5-year TCO model: cryogenic vs. mechanical (500 lb/hr baseline)
| Cost category | Cryogenic (N₂) — 5-year total | Mechanical (CO₂/NH₃) — 5-year total |
|---|---|---|
| Equipment purchase | $75,000 | $200,000 |
| Refrigerant / N₂ supply | $210,000 (est. $0.20/lb product × 210k lb/yr) | $18,000 (refrigerant top-ups) |
| Electricity | $22,000 | $85,000 |
| Planned maintenance | $12,000 | $38,000 |
| Unplanned repairs (est.) | $8,000 | $20,000 |
| 5-year TCO | $327,000 | $361,000 |
The numbers above assume 8-hour daily operation, 250 days per year, and a US average industrial electricity rate of $0.082/kWh (EIA 2026 data). At higher utilization — say, 16 hours per day — mechanical systems pull decisively ahead on TCO because nitrogen consumption scales linearly while compressor efficiency improves with load. That crossover point typically occurs around 12 hours of daily operation. Know your shift schedule before signing any purchase order.
Refrigerant transition costs in 2026
This is a line item most buyers miss entirely. R404A — still common in older commercial food freezer units — is subject to accelerating phase-down under the AIM Act. Processors buying used equipment or older model-year mechanical units should budget $8,000–$15,000 for refrigerant conversion or account for stranded asset risk. Newer units specced with CO₂ (R744) or NH₃ carry no near-term compliance risk and are the safer long-term capital choice.
US regulatory compliance: FDA, USDA, and NSF requirements
This section is conspicuously absent from nearly every competitor's content — yet for US buyers, compliance is a non-negotiable filter that should precede any other evaluation criterion.
FDA 21 CFR Part 110 and FSMA requirements
Any frozen food processing equipment installed in a US facility subject to FDA jurisdiction must comply with 21 CFR Part 110 (Current Good Manufacturing Practice) and, for covered facilities, the FSMA Preventive Controls for Human Food rule (21 CFR Part 117). For your small IQF tunnel freezer, this translates to concrete equipment specifications: all food-contact surfaces must be of food-grade material (typically 304 or 316 stainless steel), must be accessible for inspection and cleaning without tools or with commonly available tools, and must not create harborage points for microbial contamination. Verify these specifics in any equipment proposal before evaluating price.
USDA AMS and NSF/ANSI standards
Processors handling USDA-inspected products (poultry, red meat, catfish) must ensure their continuous freezer system meets USDA AMS equipment approval requirements. In practice, this means requesting documentation that the unit has been reviewed or approved for use in federally inspected establishments. NSF/ANSI Standard 2 (Food Equipment) certification is the most widely recognized third-party mark for food equipment sanitary design in the US market — look for it explicitly in supplier proposals. HACCP documentation support (critical control point data logging, temperature records) is increasingly expected by retail buyers conducting supplier audits; confirm whether the unit's control system exports HACCP-compatible records.
Application-specific settings: shrimp, blueberries, and diced chicken
Generic specs tell you what a machine can do. This section tells you how to run it. These parameters are derived from actual test runs and supplier commissioning data — the kind of application-specific guidance that's almost never included in standard buying guides.
Seafood IQF freezer settings: shrimp (26/30 count, peeled and deveined)
Target product core temperature at exit: -18°C or below. Recommended belt speed: 12–16 ft/min on a straight-belt unit. Air temperature set point: -38°C to -40°C. Air velocity: 1,800–2,200 ft/min over the product zone. Pre-crust phase on fluidized bed: activate upward air at 120% of normal velocity for the first 30% of belt length to set surface crust and prevent inter-piece adhesion. At these settings, a 10–12 g P&D shrimp typically reaches target core temp within 9–11 minutes. If your drip-loss after thaw exceeds 8%, reduce belt speed by 10% increments before adjusting temperature — freeze time, not temperature, is usually the controlling variable for shrimp yield.
Vegetable quick freeze tunnel settings: blueberries
Blueberries are one of the more forgiving products on a vegetable quick freeze tunnel — their waxy cuticle limits surface moisture and adhesion. Target belt speed: 18–22 ft/min. Air temperature: -35°C. Air velocity: 1,500–1,800 ft/min. Key watch-out: berry splitting caused by rapid surface temperature drop when berries enter a -40°C zone cold — consider a two-zone tunnel with a pre-chill entry zone at -20°C for the first 15% of belt length. Real case data from a Pacific Northwest processor showed splitting rates drop from 4.2% to 0.8% with this two-zone approach, directly improving retail pack acceptance rates.
Diced chicken (IQF protein on a compact unit)
Diced chicken (¾-inch dice, raw) presents a higher thermal mass than seafood or berries. Target core temperature: -18°C. Recommended belt speed: 8–11 ft/min. Air temperature: -40°C. Product loading density: no more than 2.5 lb/sq ft of belt surface — overloading is the single most common commissioning error on compact units. Belt loading that exceeds this threshold creates shielded zones where product in the center of the pile never achieves adequate airflow, resulting in partial freeze and food safety risk. Confirm your supplier tests at your target loading density during factory acceptance testing (FAT), not at a lower demo density.
Financing and leasing options for small US processors
For many small food processors, a $150,000–$280,000 equipment investment requires external financing. This is the purchase barrier most suppliers ignore — and the reason some buyers postpone decisions that would otherwise generate clear ROI.
SBA loan programs
The SBA 7(a) loan program can finance food processing equipment, and the SBA 504 program is particularly well-suited to fixed-asset acquisition including manufacturing equipment. Interest rates as of early 2026 track at prime plus 2.25–2.75% for 7(a) loans on equipment with a 10-year term. The application process takes 60–90 days; build this into your procurement timeline. SBA-approved lenders with food industry experience include Live Oak Bank and ReadyCap Commercial — both have funded IQF and commercial food freezer equipment acquisitions in recent years.
Equipment leasing: LEAF and Crest Capital
Operating leases through specialists like LEAF Financial (now a division of People's Capital and Leasing) or Crest Capital allow small processors to deploy a small IQF tunnel freezer with monthly payments rather than lump capital outlay. A $200,000 mechanical unit on a 60-month operating lease at current market rates runs approximately $3,800–$4,400/month. The key advantage beyond cash preservation: off-balance-sheet treatment (under ASC 842 guidance for qualifying leases) and a built-in technology upgrade path at lease end. One important caveat — food equipment leases typically require the lessee to carry commercial property insurance naming the lessor, and some agreements restrict relocation without written approval.
How to size and select the right unit for your line
Choosing a small IQF tunnel freezer without a systematic sizing process is like speccing a pump without knowing your flow rate. Here is a practical step-by-step framework used by equipment consultants when evaluating compact IQF systems for US food processors.
- Define your peak throughput requirement. Calculate your highest-demand hour across all products — not average, peak. Add a 20% safety factor. This is your nameplate capacity target.
- List all product types and geometries. If you process both shrimp and diced chicken, you need a unit configurable for both. A fluidized bed-only design may not handle your chicken SKU.
- Map available floor space. Measure not just the freezer footprint but the infeed, outfeed, and defrost access zones. NSF and USDA require minimum clearance distances around food equipment.
- Determine your daily operating hours. This single variable most directly drives the cryogenic vs. mechanical TCO crossover point identified in Section 4.
- Request factory acceptance testing (FAT) at your operating conditions. Insist on running your actual product — not a similar product — at your target belt speed and loading density before accepting delivery.
- Verify compliance documentation before issuing a PO. Request NSF certification documentation, USDA AMS acceptance letters (if applicable), and HACCP data logging capability confirmation in writing.
The IQF equipment market in 2026 includes a growing tier of well-engineered mid-range units from Asian manufacturers (particularly from China and South Korea) that are beginning to displace European brands at the entry price point. Due diligence on service network density and spare parts availability within the continental US is essential before purchasing from any brand without established domestic service infrastructure — downtime on a frozen food processing line carries a direct daily revenue cost typically ranging from $2,000 to $8,000 depending on production scale.
PAA: common questions from US buyers in 2026
What is the difference between a small IQF tunnel freezer and a blast freezer tunnel?
A blast freezer tunnel typically freezes product in batch mode on trays or racks using high-velocity cold air, resulting in clumped frozen pieces. A small IQF tunnel freezer moves product continuously on a belt, freezing each piece individually so the output is free-flowing and non-clumped. IQF output commands higher retail prices and requires less thaw preparation at the consumer or foodservice level.
How much electricity does a compact IQF freezer use?
A mechanical compact IQF freezer rated at 500 lb/hr typically draws 30–55 kW under full load. At $0.082/kWh and 8 hours/day, 250 days/year, that is approximately $5,000–$9,000 per year in electricity cost. Cryogenic units draw significantly less electricity (5–10 kW) but incur liquid nitrogen supply costs instead.
Can one small IQF tunnel freezer handle multiple product types?
Yes — most commercial food freezer systems in this class support multi-product operation via adjustable belt speed, air velocity, and temperature set points. However, allergen cross-contact and changeover cleaning time between product runs must be factored into your HACCP plan and production scheduling. Some processors run dedicated shifts per product type to minimize changeover costs.
What is the typical lead time for a small IQF tunnel freezer in the US?
As of 2026, lead times for mechanical IQF units from European and North American manufacturers run 16–26 weeks from order confirmation. Cryogenic tunnel freezers from suppliers like Messer typically ship within 8–14 weeks given their simpler construction. Budget accordingly — a 20-week lead time means Q2 orders won't support a Q3 production ramp.
Does a small IQF tunnel freezer require special facility infrastructure?
Mechanical units typically require 460V/3-phase electrical service and, for ammonia-based systems, IIAR-compliant machinery room ventilation and leak detection. Cryogenic units require bulk liquid gas supply infrastructure (dewars or bulk tanks) and adequate facility ventilation per OSHA 29 CFR 1910.146 for confined space protocols. Both types require floor drains capable of handling defrost water discharge volumes.
Frequently asked questions
Q: What does a small IQF tunnel freezer cost in the US market in 2026?
A: Cryogenic models start around $55,000–$95,000. Mechanical straight-belt and fluidized bed units range from $120,000–$210,000. Compact spiral units from premium brands like JBT can reach $280,000. Total installed cost (including electrical, refrigeration infrastructure, and commissioning) adds 15–25% to equipment price.
Q: What certifications should a small IQF tunnel freezer have for the US food market?
A: At minimum, look for NSF/ANSI Standard 2 certification for sanitary equipment design. Facilities producing USDA-inspected products need USDA AMS equipment acceptance. FDA-regulated processors must confirm compliance with 21 CFR Part 110 and FSMA Preventive Controls. Ask suppliers for written documentation of all certifications before purchase.
Q: Is a fluidized bed freezer better than a straight-belt IQF tunnel for shrimp?
A: For small, uniform shrimp (under 30 mm), a fluidized bed freezer typically delivers superior individual separation and lower inter-piece adhesion. For larger shrimp formats or high-moisture product, a straight-belt IQF tunnel with impingement airflow offers better process control and easier cleaning — both are viable depending on specific product specs.
Q: Can I finance a small IQF tunnel freezer through an SBA loan?
A: Yes. The SBA 7(a) program covers food processing equipment, with 10-year terms and competitive rates. The SBA 504 program is best for larger fixed-asset purchases. Expect 60–90 day approval timelines. Equipment leasing through LEAF Financial or Crest Capital is a faster alternative with monthly payment structures starting around $3,800–$4,400/month for a $200,000 unit on a 60-month term.
Q: How long does it take to install and commission a small IQF tunnel freezer?
A: Installation and commissioning for a mechanical small IQF tunnel freezer typically takes 5–10 business days for a pre-assembled compact unit, assuming all site infrastructure (electrical, refrigeration, drainage) is ready. Allow an additional 2–3 days for product-specific FAT runs and operator training. Cryogenic units generally commission faster — 2–4 days — due to simpler mechanical scope.
Selecting the right small IQF tunnel freezer for your US facility is ultimately a multi-variable optimization: throughput vs. footprint, capital cost vs. operating cost, product flexibility vs. sanitation simplicity. The brand comparison table, TCO model, compliance checklist, and application-specific parameters in this guide are designed to compress that evaluation process from months to weeks. Use the sizing framework in Section 8 as your internal decision document, and require suppliers to respond to each criterion in writing — a supplier who can't answer your FAT protocol question in detail is one whose commissioning support you will be calling at 2 a.m. after a failed production run.
Keywords:
Inquiry
If you are interested in our products, please leave your email to receive a free product quote, thank you!
More information
Tel:
Sales E-mail: