Impingement tunnel freezer guide: how it works, key features & selection tips
Release Time:
Aug 30,2026
Author:

Article overview
A technical and commercial deep-dive into impingement tunnel freezers for US food manufacturers. Covers working principles, product benchmarks, TCO, AIM Act refrigerant compliance, USDA/NSF sanitation standards, and plant integration — everything needed to evaluate and specify a system in 2026.
Table of contents
- 1. What is an impingement tunnel freezer?
- 2. How impingement jet freezing works: the physics explained
- 3. Performance benchmarks: freezing curves for common US products
- 4. TCO analysis: impingement vs. spiral vs. fluidized bed freezers
- 5. US regulatory and food safety compliance
- 6. Refrigerant selection guide for the US market
- 7. Integration and automation in modern food plants
- 8. How to select the right impingement tunnel freezer
- 9. FAQ
What is an impingement tunnel freezer?
An impingement tunnel freezer is a continuous industrial freezing system that directs high-velocity jets of cold air — typically at 30–60 m/s — from nozzle arrays positioned above and below a moving conveyor belt, rapidly stripping the insulating boundary layer from food surfaces and achieving freezing speeds 3–5× faster than conventional blast freezer tunnel designs.
That single capability — aggressive boundary-layer disruption — is what separates impingement technology from every other airflow freezing technology in use today. The principle sounds straightforward, but the engineering behind a well-designed system is anything but simple.
Where does it fit in the freezing equipment landscape?
Industrial food processors have several continuous freezing system options: spiral freezers, fluidized bed IQF tunnels, plate freezers, cryogenic (LN₂ or CO₂) systems, and impingement tunnels. Each serves a different product profile. The impingement tunnel freezer occupies a well-defined niche — flat, thin, or coated products where surface area is large relative to mass. Think burger patties, fish fillets, chicken tenders, pizza crusts, and breaded shrimp. For those geometries, no mechanical alternative delivers the same freeze speed without the capital cost of a nitrogen impingement freezer.
Key variants available in 2026
The market now offers five main configurations. Single-pass straight-through units are the workhorses of high-throughput burger and fish lines. Multi-pass designs fold the belt to reduce footprint — practical for plants where floor space costs more than energy. Combination impingement IQF systems handle initial crust freezing followed by through-freezing in a single enclosure. Nitrogen impingement freezers pair LN₂ injection with high-velocity jets for ultra-fast surface set on premium products. Finally, hygienic-design variants are engineered from the ground up for USDA and EHEDG compliance, with tool-free nozzle removal, full-open access panels, and sloped floors for complete drainage.
How impingement jet freezing works: the physics explained
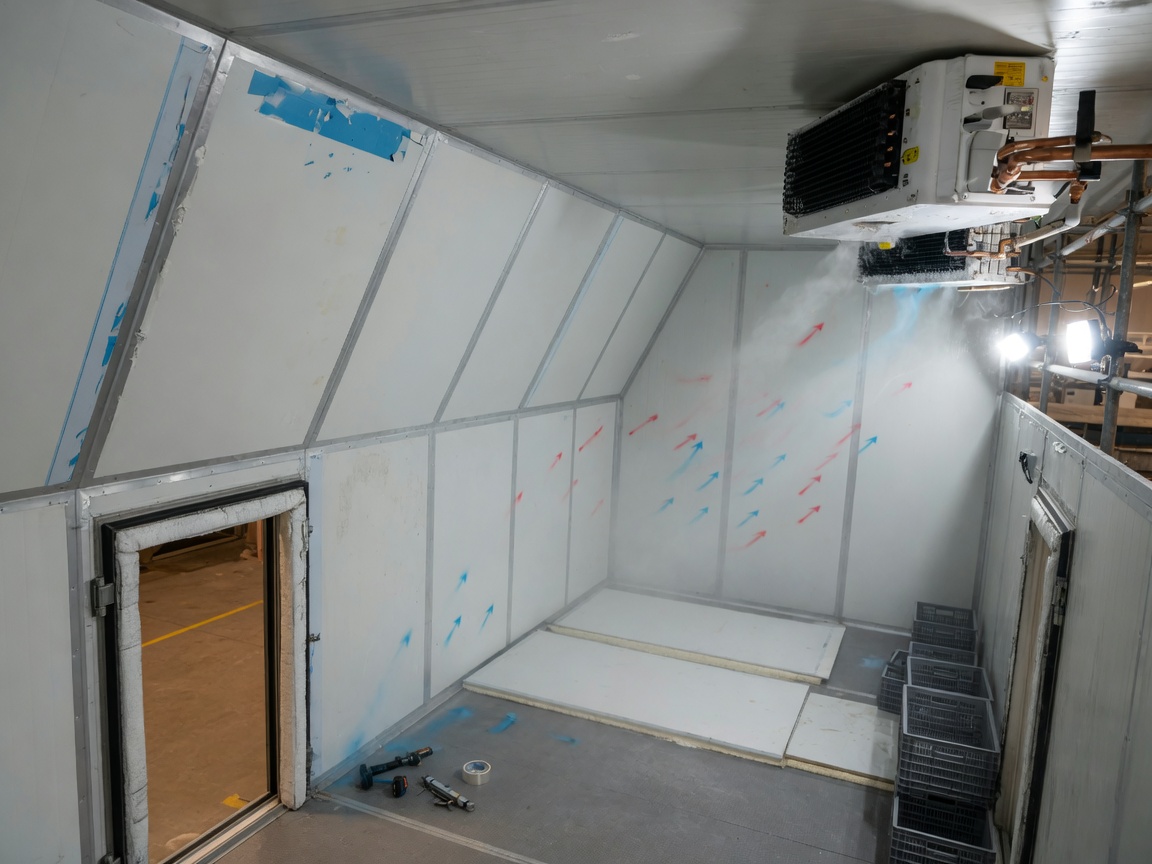
The core mechanism is heat transfer coefficient elevation through forced convection. Standard blast freezer tunnel designs move air at 5–12 m/s across a product surface. That airflow is laminar near the product, creating a stagnant thermal boundary layer — essentially an insulating blanket of warmed air that the refrigerant must fight through. Impingement jet freezing eliminates that blanket entirely.
The boundary-layer principle
Nozzle arrays — typically spaced 100–200 mm apart — fire perpendicular jets at the product surface. On impact, each jet fans outward radially, creating turbulent flow that continuously refreshes the cold air in contact with food. Heat transfer coefficients in impingement systems routinely reach 80–150 W/(m²·K), compared with 20–40 W/(m²·K) in a conventional tunnel. That is not a marginal improvement. It is the difference between freezing a 12 mm fish fillet in 4 minutes versus 10 minutes.
Why do so many food engineers underestimate this? Because published specs from legacy equipment manufacturers still reference airspeed at the fan outlet, not at the product surface — a misleading figure that overstates apparent performance.
Crust freezing and IQF quality
One of the most practical benefits of impingement is crust freezing — forming a rigid, frozen surface crust in 60–120 seconds before the product center reaches 0°C. This matters enormously for coated products: a frozen crust locks the breading or batter in place before it can slump, detach, or absorb moisture from adjacent pieces. It also enables individual quick freezing (IQF) of items that would otherwise stick together on a standard conveyor belt, such as marinated chicken pieces or glazed seafood portions. Just as a flash-hardened shell protects a soft interior, the crust acts as structural scaffolding for the rest of the freeze cycle.

Performance benchmarks: freezing curves for common US products
Data matters more than marketing copy. The table below consolidates 2026 performance benchmarks drawn from equipment commissioning reports and processing line audits across US food plants. All values assume an evaporator temperature of −40°F (−40°C) and belt loading of 8–12 kg/m².
| Product | Thickness | Impingement dwell time | Standard blast tunnel | Time saved | Exit core temp |
|---|---|---|---|---|---|
| Burger patty (4 oz) | 12 mm | 4.5 min | 10–12 min | ~55% | 0°F (−18°C) |
| Chicken tender (breaded) | 18 mm | 7 min | 14–16 min | ~52% | 0°F (−18°C) |
| Fish fillet (cod, 3/4 in) | 19 mm | 6.5 min | 13–15 min | ~53% | 0°F (−18°C) |
| Pizza (10-inch, topped) | 25 mm total | 9 min | 18–22 min | ~50% | 0°F (−18°C) |
| Shrimp (3/4-in, glazed) | 19 mm | 5 min | 8–9 min | ~40% | 0°F (−18°C) |
Real-world case: Midwest seafood processor
According to real-world case data from a Midwest US seafood processing facility, switching from a standard blast freezer tunnel to an impingement IQF processing line cut freeze times by 35% on 3/4-inch shrimp. More significantly, IQF separation quality improved — product sticking rates dropped from roughly 8% of throughput to under 1%, reducing downstream rework labor by an estimated $180,000 per year. These are the numbers that justify CapEx approval.
When impingement is not the right call
Of course, there are situations where alternatives outperform. Irregular bulk items — diced vegetables, whole shrimp, peas — freeze more uniformly in a fluidized bed IQF system where air lifts and tumbles individual pieces. An impingement tunnel freezer applied to those products would produce uneven freeze depth and potential surface dehydration. The technology excels at what it was designed for; forcing it into the wrong application is an expensive mistake.
TCO analysis: impingement vs. spiral vs. fluidized bed freezers
Upfront CapEx is only part of the story. For a 10-year ownership horizon, energy and maintenance costs routinely account for 60–70% of total cost of ownership (TCO). Evaluating a quick freeze tunnel system purely on purchase price is one of the most common — and costly — procurement errors in the industry.
Upfront CapEx comparison
A mid-capacity impingement tunnel freezer (2,000–3,000 lb/hr throughput) carries a typical installed cost of $350,000–$600,000 in the current US market. A comparable spiral freezer alternative runs $500,000–$900,000 due to structural complexity and larger refrigeration plant requirements. Fluidized bed IQF units for comparable throughput land in the $400,000–$700,000 range. On CapEx alone, impingement often wins — but the operating cost picture is more nuanced.
Energy, maintenance, and 10-year TCO
High-velocity fans consume significant electricity. An impingement system running at full capacity typically draws 15–25 kWh per metric ton of product frozen — higher than a spiral freezer at 12–18 kWh/MT for the same throughput, because impingement fans run at higher static pressure. However, the shorter dwell time means the refrigeration plant runs at peak load for less time per unit of product, partially offsetting fan energy. Maintenance costs favor impingement: fewer moving parts than a spiral (no large rotating drum), and modern hygienic designs reduce CIP/COP cleaning time from 4–6 hours to under 2 hours per shift, cutting labor cost and downtime losses. Over 10 years and at $0.10/kWh (US industrial average), the energy difference between impingement and spiral narrows to under $80,000 for a mid-size plant — often less than one year of avoided maintenance labor. That makes TCO highly site-specific; any responsible vendor should model it with your actual production schedule and utility rates.
"When evaluating freezing equipment, the purchase price is the entry ticket, not the total cost. Energy, sanitation labor, downtime, and yield loss over a 10-year horizon typically exceed CapEx by a factor of two or more for high-utilization lines." — ASHRAE Refrigeration Handbook, Food Processing chapter
US regulatory and food safety compliance
For American food processors, regulatory compliance is not optional — it is a prerequisite for operating. An impingement tunnel freezer installed in a USDA-inspected facility must meet specific sanitation, equipment certification, and design standards that are stricter than general commercial food freezer requirements.
USDA/FSIS sanitation and NSF/ANSI certification
USDA Food Safety and Inspection Service (FSIS) regulations require that all food-contact surfaces in federally inspected meat and poultry plants be constructed of corrosion-resistant, non-absorbent materials capable of withstanding repeated sanitation. NSF/ANSI 2 (Food Equipment) certification provides the most recognized third-party verification that a freezer meets these requirements. When specifying a system, confirm that the conveyor belt, nozzle assemblies, belt support frames, and drain channels all carry NSF/ANSI 2 certification — not just the outer enclosure.
Beyond materials, FSIS expects equipment to be designed for effective cleaning in place (CIP) or cleaning out of place (COP). Practical CIP/COP design considerations include: fully drainable sumps with no pooling zones, nozzle arrays that swing out or detach without tools, belt tracking systems accessible without disassembly, and smooth-radius interior corners (minimum 3 mm) that prevent biofilm accumulation. Some crust freezing machine designs still use corrugated internal panels for structural rigidity — those are incompatible with FSIS expectations and should be rejected during specification review.
HACCP integration and temperature verification
A continuous freezing system operating as a Critical Control Point (CCP) — for example, achieving a lethal or limiting step for pathogen control — must have validated time-temperature documentation. Modern impingement tunnel freezers with integrated data-logging PLCs can export continuous belt speed, air temperature, and product core temperature records directly to HACCP management software. This is not a luxury feature; it is quickly becoming an expectation from major retail and QSR customers conducting supplier audits.
Refrigerant selection guide for the US market
The refrigerant question has become one of the most consequential decisions in freezer procurement, and the regulatory landscape is shifting rapidly. Getting this wrong in 2026 can mean a system that is legally obsolete or commercially stranded within its expected service life.
HFC phase-down under the AIM Act
The American Innovation and Manufacturing (AIM) Act mandates an 85% reduction in HFC production and consumption by 2036 relative to a 2011–2013 baseline. High-GWP refrigerants commonly used in legacy industrial food processing freezer systems — R404A (GWP 3,922) and R507A (GWP 3,985) — are already subject to allocation restrictions and price premiums. Purchasing an impingement tunnel freezer designed around R404A in 2026 is a financially risky decision: refrigerant supply will tighten further, insurance costs are rising, and retrofit to lower-GWP alternatives carries significant engineering cost.
Natural refrigerants: CO₂ and ammonia
The mainstream replacement path for US industrial freezer applications now runs through two natural refrigerants. Ammonia (R717, GWP = 0) remains the gold standard for large centralized systems above 500 kW capacity — superior thermodynamic efficiency, very low operating cost, but requiring OSHA PSM compliance above 10,000 lb charge. CO₂ (R744, GWP = 1) in transcritical or cascade configurations is gaining rapid adoption in mid-size impingement tunnel installations, particularly where ammonia charge limits or urban siting constraints apply. ROI timelines for transitioning from R404A to CO₂ cascade typically run 4–6 years based on 2026 US utility and refrigerant pricing.
Cryogenic (LN₂/CO₂) trade-offs
Food cryogenic freezing equipment — specifically nitrogen impingement freezers — offers unmatched freeze speed and minimal footprint, at the expense of ongoing liquid nitrogen supply cost. For high-value proteins or when floor space is genuinely constrained, LN₂ impingement can deliver ROI positive outcomes. At current US LN₂ spot prices (~$0.12–$0.18/lb), a cryogenic system processing 1,000 lb/hr of chicken tenders carries consumable costs of roughly $18–$25 per operating hour — versus $4–$7/hr in electricity for a mechanical equivalent. The crossover point depends on plant utilization rate; for operations running fewer than 6 hours per day, cryogenic sometimes wins on TCO.
Integration and automation in modern food plants
An impingement tunnel freezer does not operate in isolation. Its true value is realized — or lost — based on how well it connects with upstream portioning equipment and downstream packaging lines.
Upstream integration: portioning and forming lines
In a modern burger patty line, a forming machine deposits patties onto a transfer conveyor at rates of 150–300 pieces per minute. The impingement tunnel inlet must match this cadence without creating gaps or overlaps on the belt — both reduce freezing uniformity and throughput efficiency. Variable-speed belt drives synchronized via PLC handshake with the former are the standard solution. Lane guides at the inlet ensure consistent product spacing and prevent edge-crowding, which causes localized warm zones in airflow freezing technology systems.
Downstream integration: packaging and metal detection
At the tunnel exit, product temperature must be stable and uniform before entering packaging equipment. A freezing conveyor belt system that delivers products with a ±3°F core temperature variance will cause condensation and clumping in vacuum packaging lines. Exit temperature monitoring with automatic belt-speed feedback correction — now standard on AI-enabled systems — addresses this directly. Metal detection and checkweighing stations are typically positioned 6–10 feet downstream of the exit to allow slight thermal equilibration before inspection. Integration with downstream WMS or ERP systems via OPC-UA protocol is increasingly requested by Tier 1 US food manufacturers.
2026 smart controls and energy optimization
AI-assisted control platforms now deployed on leading impingement tunnel freezer models use real-time sensor arrays — product surface temperature IR cameras, belt load cells, and evaporator pressure transducers — to continuously optimize fan speed, belt velocity, and defrost cycles. According to near-term operational data from early adopters, these systems reduce energy consumption by 10–20% versus fixed-parameter operation, with no measurable impact on IQF quality outcomes. That is meaningful at scale: a plant running 16 hours per day, 300 days per year could save $40,000–$90,000 annually on electricity alone.
How to select the right impingement tunnel freezer
Selection mistakes are expensive and difficult to reverse once a system is installed. The following structured process reflects best practice for US food plant procurement teams evaluating an impingement tunnel freezer in 2026.
Step-by-step selection process
- Define your product envelope: Document the full range of products — thickness, weight, coating type, initial temperature — that will run on the system. A system sized for your thinnest product will underfreeze your thickest one.
- Calculate required throughput: Work backward from finished-goods production targets, accounting for yield loss, line efficiency, and planned downtime. Add a 15–20% capacity buffer for future volume growth.
- Specify the refrigerant upfront: Given AIM Act timelines, specify CO₂ cascade or ammonia from the outset unless a compelling cryogenic business case applies. Do not accept R404A designs without a written upgrade path.
- Require NSF/ANSI 2 documentation and CIP validation: Request documented sanitation validation protocols, not just a checklist. Ask for reference site contacts at USDA-inspected plants running the same model.
- Request product-specific freezing trials: Reputable suppliers of quick freeze tunnel systems will run your actual product — under NDA if needed — and provide documented freezing curves before you commit CapEx.
- Model 10-year TCO with your utility rates: Use your actual electricity cost per kWh and sanitation labor rate. A spreadsheet from the vendor is a starting point; validate it independently.
- Evaluate controls and data connectivity: Confirm OPC-UA or equivalent protocol support, HACCP data export format, and remote diagnostics capability before finalizing the specification.
Common selection mistakes to avoid
Selecting based on airspeed at the fan rather than measured heat transfer coefficient at the product surface is the most pervasive technical error. On the commercial side, accepting a standard blast freezer tunnel with impingement branding — some vendors apply the term loosely to any high-velocity tunnel — without verifying nozzle-to-product distance and jet geometry is a specification risk. Finally, underestimating sanitation complexity for multi-product lines that switch between allergen-containing and allergen-free SKUs can create both regulatory exposure and unplanned downtime.
Frequently asked questions
Q: What products are best suited for an impingement tunnel freezer?
A: Impingement tunnel freezers deliver peak performance on flat or thin products with a high surface-area-to-mass ratio — burger patties, breaded chicken tenders, fish fillets, pizza crusts, and coated seafood. For irregular bulk items like diced vegetables or whole shrimp, a fluidized bed IQF system typically produces more uniform individual quick freezing results.
Q: How does an impingement tunnel freezer compare to a spiral freezer?
A: Impingement units freeze thin products 40–60% faster, have lower CapEx, and require less floor space than spiral freezer alternatives. Spiral freezers handle a broader product mix — including thicker or irregularly stacked items — and carry lower fan energy consumption per ton. TCO over 10 years is comparable for high-utilization lines; the right choice depends on your specific product range and plant layout.
Q: What refrigerant should I specify for a new impingement tunnel freezer in the US?
A: In 2026, CO₂ (R744) cascade systems and ammonia (R717) are the recommended choices given AIM Act HFC phase-down requirements. Avoid R404A and R507A for new installations — supply restrictions and rising costs will erode ROI within the equipment's service life. For cryogenic applications, LN₂ impingement remains viable for high-value, low-volume production.
Q: What certifications should I require for a USDA-inspected plant?
A: Require NSF/ANSI 2 certification on all food-contact components, documented CIP/COP sanitation validation, and confirmation that the design meets USDA FSIS sanitation construction standards. Request reference contacts at currently operating USDA-inspected facilities running the same equipment model before finalizing procurement.
Q: How much energy does an impingement tunnel freezer consume?
A: Typical energy consumption is 15–25 kWh per metric ton of product frozen, varying with fan speed settings, evaporator temperature, and product load. AI-enabled smart control systems available in 2026 can reduce this by 10–20% through dynamic parameter optimization. Always model energy cost using your plant's actual utility rate, not national averages.
In summary, the impingement tunnel freezer remains one of the most effective tools available to US food manufacturers needing rapid, high-quality freezing for flat and thin products. The 2026 procurement decision is more complex than it was a decade ago — AIM Act refrigerant compliance, USDA sanitation expectations, and AI-driven automation have all raised the specification bar. But the core value proposition is unchanged: faster freezing, better IQF quality, and a competitive total cost of ownership when properly matched to product and production requirements. Use the benchmarks, TCO framework, and selection checklist in this guide to evaluate suppliers rigorously — and require product-specific freezing trial data before any capital commitment.
Keywords:
Inquiry
If you are interested in our products, please leave your email to receive a free product quote, thank you!
More information
Tel:
Sales E-mail: