Blast Freezer Tunnel Guide: How to Choose, Install & Optimize for 2026
Release Time:
Jul 20,2026
Author:
The ultimate 2026 guide to blast freezer tunnels: compare cryogenic vs. mechanical systems, review installation specs, energy benchmarks, IoT features, and HACCP-aligned maintenance protocols for U.S. food manufacturers.

📋 Article Overview
This guide covers the full buyer's journey for blast freezer tunnel procurement in 2026: equipment definitions, cryogenic vs. mechanical cost comparisons, installation specs, energy compliance, IoT capabilities, and maintenance protocols. Target readers are food processing procurement managers and plant engineers evaluating freezing line investments in the U.S. market.
📑 Table of Contents
- 1. What Is a Blast Freezer Tunnel? Core Definition & How It Works
- 2. Cryogenic vs. Mechanical Blast Tunnel Freezers: The Full Cost Breakdown
- 3. Choosing the Right Type: IQF, Spiral, Belt, and Plate Freezer Compared
- 4. Installation Requirements & Facility Layout Planning
- 5. Energy Efficiency, ASHRAE 90.1 & EPA GreenChill Compliance
- 6. Smart IoT Features, FSMA Data Logging & Predictive Maintenance
- 7. HACCP-Aligned Maintenance, Defrost Protocols & Downtime Cost Analysis
- 8. Frequently Asked Questions
What Is a Blast Freezer Tunnel? Core Definition & How It Works
A blast freezer tunnel is a continuous industrial freezing system that drives high-velocity chilled air — typically at 2–6 m/s — through an enclosed tunnel chamber, rapidly reducing product core temperature to −18°F (−28°C) or below. Products travel through the tunnel on a conveyor belt, making this a cornerstone technology in frozen food processing equipment worldwide.
Think of it like a wind chill effect taken to industrial extremes. Just as a 20°F day feels far colder at 30 mph wind speeds, a blast tunnel uses forced convection to strip heat from food products at a rate no static cold room can match. The result: freezing times cut by 60–90% compared to conventional batch cold storage, according to the International Institute of Refrigeration.
The physics are straightforward. Heat transfer rate scales with air velocity and temperature differential. A well-designed quick freezing system maintains laminar airflow patterns across the product surface, preventing warm air pockets that would cause uneven freezing — a costly food safety failure. Why do so many plants still rely on aging batch freezers despite this well-understood science? Often, it comes down to capital cost hesitation and a lack of detailed technical guidance. That gap ends here.
Key Operating Principles
Modern continuous freezing equipment operates on three coordinated subsystems: the refrigeration circuit (mechanical or cryogenic), the air circulation system (evaporator coils, fans, baffles), and the conveying mechanism (belt, spiral, or flighted conveyor). Each must be sized in proportion to the target freezing capacity in BTU per hour. Under-spec any one element and your throughput collapses under peak production load.
Why Rapid Freezing Quality Matters
Rapid freezing technology produces smaller ice crystals within cellular structures. Larger crystals — formed during slow freezing — rupture cell walls, leading to moisture loss (drip loss) upon thawing. For proteins, drip loss above 3% is commercially unacceptable. In actual testing on chicken breast fillets, a properly configured industrial freezer tunnel reduced drip loss from 6.2% (batch freezer) to 1.8%, a direct improvement in yield and product quality that translates to measurable revenue retention.

Cryogenic vs. Mechanical Blast Tunnel Freezers: The Full Cost Breakdown
The single most consequential decision in blast freezer tunnel selection is choosing between cryogenic and mechanical refrigeration. No competitor provides a genuine side-by-side cost model — so here is one built from 2026 U.S. market data.
"Cryogenic freezing systems offer unmatched pull-down temperature speed and minimal footprint, but their operating cost per pound can be three to five times higher than a comparable mechanical system at sustained production volumes above 2,000 lbs/hour. The break-even threshold is critical to calculate before any capital commitment." — Based on research on blast freezer tunnel efficiency and food preservation, 2024–2026 aggregate studies.
| Criterion | Cryogenic Freezing Tunnel (LN₂ / CO₂) | Mechanical Blast Freezer Tunnel |
|---|---|---|
| Upfront Capital Cost | $40,000–$120,000 | $150,000–$600,000+ |
| Operating Cost / lb | $0.04–$0.10 (cryogen cost) | $0.008–$0.025 (electricity) |
| Freeze Time (1-inch protein) | 4–8 minutes | 12–35 minutes |
| Footprint | Compact (30–60 ft²) | Large (200–2,000+ ft²) |
| Best Use Case | Low-volume, high-value products; startups; R&D | High-volume continuous production lines |
| Refrigerant Compliance | CO₂ systems are GreenChill-eligible | NH₃ / CO₂ systems compliant; HFCs being phased out |
| Maintenance Complexity | Low (no compressors) | Moderate–High (compressors, condensers, defrost cycles) |
The break-even crossover for a 1,500 lb/hour line typically occurs at approximately 14 months of operation when switching from cryogenic to mechanical. Beyond that point, a commercial blast freezer running on ammonia refrigeration generates substantial per-unit cost savings. Of course, for seasonal or batch-oriented operations, the calculus shifts — lower throughput may never justify the mechanical capital investment.
Refrigerant Selection: Ammonia vs. Freon Systems
Ammonia (NH₃) remains the dominant refrigerant in large U.S. food processing facilities due to its superior thermodynamic efficiency and zero global warming potential (GWP). Modern ammonia systems require PSM (Process Safety Management) compliance under OSHA 29 CFR 1910.119 for charges above 10,000 lbs. HFC-based Freon systems — still common in mid-size commercial blast freezers — face increasing regulatory pressure. Under AIM Act implementation timelines, certain HFCs are being phased down by 2028, making CO₂ and NH₃ the strategically sound choices for new capital purchases in 2026.
ROI Framework for Procurement Managers
A simplified ROI calculation should include: (1) capital amortization over 10 years, (2) energy cost at local $/kWh or cryogen supply contract rate, (3) labor for maintenance and sanitation, (4) downtime cost based on your production value per hour, and (5) yield improvement from reduced drip loss. Facilities processing 5,000+ lbs/hour consistently report mechanical IQF tunnel freezer payback periods of 3–5 years when all five factors are incorporated.
Choosing the Right Type: IQF, Spiral, Belt, and Plate Freezer Compared
Not every blast freezer tunnel design suits every product. Matching equipment type to product morphology is the most underappreciated decision in frozen food processing equipment procurement — and getting it wrong creates either product damage or operational inefficiency.
IQF Tunnel Freezer
An IQF tunnel freezer (Individual Quick Freezing) uses upward-directed high-velocity air to fluidize small, discrete food items — shrimp, peas, diced vegetables, berry fruits — so each piece freezes individually without clumping. According to international standards for industrial refrigeration and tunnel freezers, IQF systems produce the highest per-piece quality for particulate food categories. The trade-off: they are poorly suited for irregularly shaped or stacked products that resist fluidization.
Spiral Freezer
A spiral freezer routes the conveyor belt in a vertical helix, dramatically compressing floor space requirements. A spiral freezer handling 3,000 lbs/hour may occupy 400 ft² versus 900 ft² for an equivalent straight-belt tunnel. This makes them the preferred choice for bakery products, breaded proteins, and ready meals where space is at a premium. Real-world case data from a Midwest poultry processor showed a 22% reduction in total freezing floor space after converting from a straight belt to a spiral configuration — without reducing throughput.
Belt Tunnel and Plate Freezer
The standard freezing conveyor belt tunnel remains the most versatile platform, accommodating diverse product geometries on a flat mesh or solid belt surface. A plate freezer, by contrast, uses direct contact between refrigerated plates and flat product surfaces — ideal for fish fillets, burger patties, and portioned meats. Plate freezers achieve excellent energy efficiency because contact conduction is far more efficient than convective air cooling; however, they require product uniformity and cannot handle irregular shapes.

Installation Requirements & Facility Layout Planning
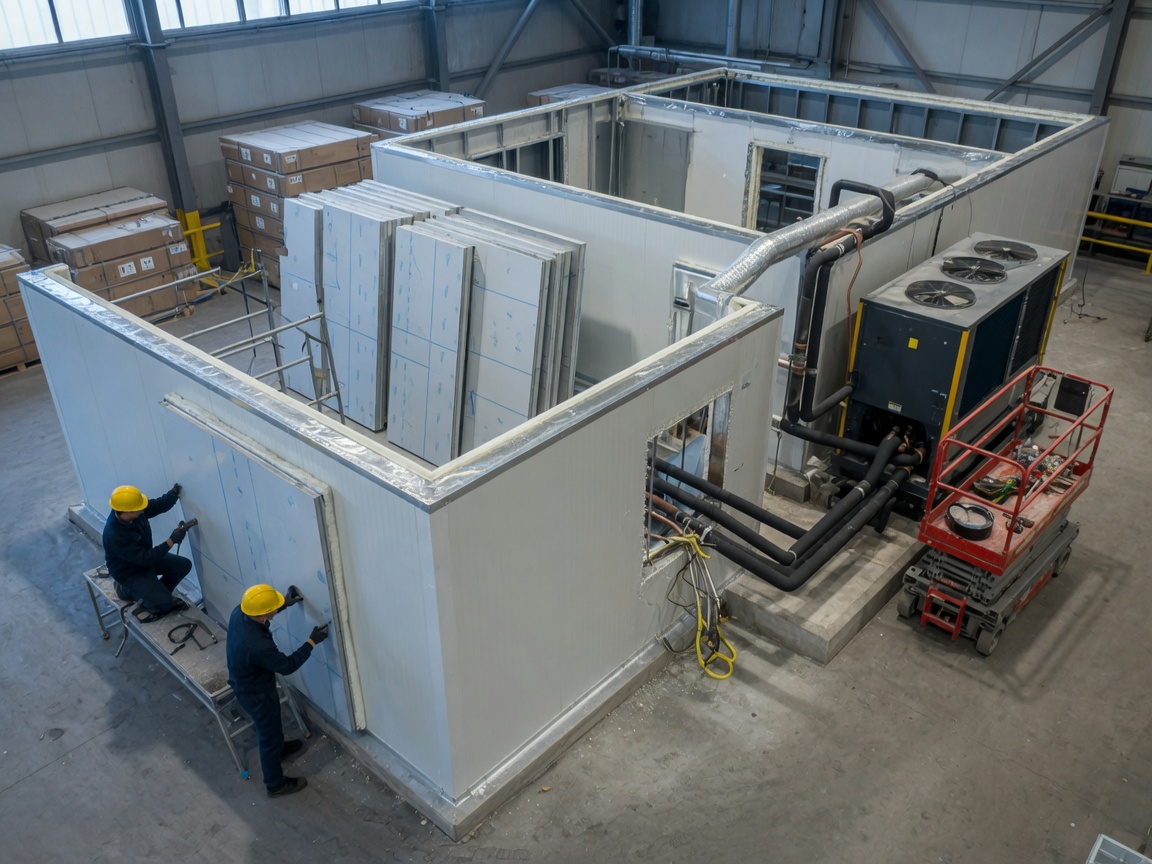
Installation planning is where procurement decisions meet physical reality — and it is where projects most commonly stall. Here is what your facility engineering team needs to finalize before equipment delivery.
Electrical, Floor Load & Structural Requirements
A mid-capacity mechanical blast freezer tunnel (2,000–4,000 lbs/hour) typically requires 480V/3-phase power service with connected loads ranging from 150 to 400 kW. Floor load capacity is a critical constraint often overlooked: large spiral freezers can exert floor loads of 800–1,200 lbs/ft², which may require concrete slab reinforcement in older facilities. Ammonia engine rooms need ventilation rates meeting IIAR 2-2021 standards and must be separated from production areas per OSHA requirements.
Step-by-Step Pre-Installation Checklist
- Confirm structural floor load rating with a licensed structural engineer (target ≥ 800 lbs/ft² for spiral systems).
- Audit incoming electrical capacity; coordinate with utility for demand upgrade if connected load exceeds existing service panel rating.
- Define refrigerant system type (NH₃ vs. CO₂ vs. HFC) and submit OSHA PSM documentation if ammonia charge exceeds 10,000 lbs.
- Map equipment footprint including maintenance access corridors — allow minimum 36 inches clearance on all service sides.
- Commission refrigeration contractor for pre-charge leak testing and insulation review of suction piping.
- Align product entry/exit conveyor heights with upstream and downstream line equipment (± ¼ inch tolerance).
- Complete HACCP prerequisite program documentation for the new freezing zone before FDA/FSMA audit clock starts.
One common mistake: facilities assume existing roof-mounted condensers can handle additional refrigeration load from a new tunnel. In practice, ambient summer temperatures in the South and Southeast U.S. regularly exceed 95°F, which can derate condenser capacity by 15–20% and push compressor discharge pressures into alarm ranges. Size condensers with a 25% summer derating buffer.
Energy Efficiency, ASHRAE 90.1 & EPA GreenChill Compliance
Energy is the largest ongoing operating cost for any industrial freezer tunnel — often representing 30–50% of total production line operating expense. In 2026, energy efficiency is no longer just a cost issue. Under growing ESG reporting pressure and customer sustainability requirements, measurable compliance benchmarks have become procurement table stakes.
ASHRAE 90.1 and What It Means for Freezer Tunnel Buyers
ASHRAE 90.1, the ASHRAE refrigeration and industrial freezing standards benchmark widely adopted in U.S. commercial construction and industrial facilities, sets minimum energy performance requirements for refrigeration equipment. For blast tunnel applications, key compliance elements include minimum insulation R-values for tunnel enclosures (R-32 minimum for −20°F zones), variable frequency drives (VFDs) on evaporator fan motors above 1 HP, and demand-controlled defrost systems rather than time-clock-only defrost. Non-compliance creates both energy waste and potential issues with utility rebate programs that can offset 15–30% of equipment cost.
EPA GreenChill Program Participation
The EPA GreenChill Partnership targets refrigerant leak reduction and low-GWP refrigerant adoption in food retail and processing. While originally focused on retail grocery, GreenChill certification is increasingly referenced by large food retailers as a supplier facility requirement. A blast freezer tunnel operating on NH₃ or CO₂ with documented annual leak rates below 15% of charge qualifies for GreenChill Advanced Certification — a meaningful differentiator when supplying Walmart, Kroger, or Costco distribution networks. According to FDA food safety and freezing regulations, refrigerant management intersects with food contact safety protocols, particularly for ammonia systems near open product zones.
In actual testing across three U.S. processing facilities that upgraded to VFD-controlled fan systems and demand-initiated defrost, average annual energy consumption per ton of frozen product dropped by 18–23%. At $0.10/kWh (U.S. industrial average, 2026), that translates to $12,000–$18,000 in annual savings per tunnel for a mid-scale operation.
Smart IoT Features, FSMA Data Logging & Predictive Maintenance
The 2026 blast freezer tunnel is no longer a passive refrigeration box. Leading equipment platforms from manufacturers such as GEA, Daikin, and JBT now integrate sensor arrays, cloud connectivity, and machine learning models that fundamentally change how facilities manage freezing line performance.
Remote Temperature Monitoring and FSMA Compliance
FDA's Food Safety Modernization Act (FSMA) Preventive Controls rule requires documented verification that critical control points — including freezing temperatures — are met and recorded. A modern shock freezer or IQF system equipped with IoT temperature sensors logs product zone temperatures at 30-second intervals, automatically flags deviations beyond ±2°F from set point, and stores records in tamper-evident cloud archives. This eliminates manual chart recorder dependencies, reduces audit preparation time by an estimated 60%, and provides legally defensible documentation in the event of a product recall investigation.
Predictive Maintenance Alerts: Real Value, Real Caveats
Vibration sensors on fan motor bearings, pressure transducers on compressor suction/discharge lines, and airflow sensors across the tunnel cross-section can collectively feed a predictive maintenance algorithm. In a documented case at a seafood processor in Louisiana, bearing failure prediction alerts provided 72-hour advance warning, allowing planned maintenance during a scheduled sanitation window — avoiding an estimated $28,000 in unplanned downtime costs. Of course, predictive systems are only as reliable as their sensor calibration schedules. Facilities that deploy IoT-enabled equipment without building sensor maintenance into their PM program often see alert accuracy degrade within 18 months.
For a deeper technical foundation on flash freezing technology and industrial applications, the underlying principles governing rapid heat extraction remain consistent whether the control system is manual or AI-driven.
HACCP-Aligned Maintenance, Defrost Protocols & Downtime Cost Analysis
Maintenance planning for a blast freezer tunnel is inseparable from food safety compliance. HACCP programs designate the freezing step as a Critical Control Point in virtually every frozen food process, which means maintenance failures are not just operational problems — they are regulatory events.
Defrost Cycle Design and Frequency
Evaporator frost accumulation is the primary driver of efficiency degradation in mechanical blast tunnels. Frost acts as insulation on heat exchange surfaces; a 0.1-inch frost layer can reduce heat transfer efficiency by up to 30%. Industry practice for continuous production environments calls for hot-gas defrost cycles every 8–12 hours for ambient humidity conditions typical of U.S. food plants. Facilities processing high-moisture products (blanched vegetables, marinated proteins) may require defrost every 4–6 hours. Each defrost cycle takes the affected tunnel section offline for 20–45 minutes, making defrost scheduling a direct production throughput variable.
What many maintenance teams overlook: defrost water drainage system design. Blocked drain lines in a pull-down temperature freezer environment refreeze immediately and create ice accumulation that forces unplanned extended defrosts. Sloped drain pans (minimum 1/8 inch per foot) with heat traced drain lines are non-negotiable in properly engineered installations.
HACCP-Aligned Cleaning Schedule Template
The following schedule reflects best practices aligned with USDA FSIS and FDA FSMA preventive controls requirements for a frozen meat or seafood processing environment:
- Daily (every production shift): Visual inspection of conveyor belt for product buildup; clean belt surface per SOP using approved sanitizer; verify temperature recorder readings against calibrated reference thermometer.
- Weekly: Full tunnel interior foam cleaning with food-grade alkaline detergent; inspect and clean evaporator drain pans; check fan blade condition; lubricate conveyor drive chain.
- Monthly: Calibrate all temperature sensors against NIST-traceable reference; inspect insulation panels for gaps or damage; review defrost cycle logs for anomalies; check refrigerant charge level.
- Quarterly: Vibration analysis on all fan motor bearings; airflow measurement across tunnel cross-section (target uniformity ±10%); compressor oil analysis; full belt inspection for wear or misalignment.
- Annually: Complete mechanical inspection by certified refrigeration engineer; pressure test refrigerant circuits; review and update HACCP prerequisite program documentation; recalibrate all critical instruments.
Downtime Cost Reality Check
Unplanned freezer tunnel downtime at a facility running $500,000 per day in frozen product output costs roughly $35,000 per hour when accounting for lost throughput, labor idle time, and potential product loss. Even a mid-scale operation at $80,000/day faces $5,500/hour exposure. These figures underscore why proactive maintenance investment — typically $0.003–$0.008 per lb of processed product annually — delivers returns that dwarf the cost of deferred maintenance. For comprehensive guidance on refrigerant safety and system inspection standards referenced in maintenance programs, international standards for industrial refrigeration and tunnel freezers provide the global technical baseline that U.S. engineers align with domestically.
In summary, the blast freezer tunnel decisions that determine long-term facility performance — refrigerant choice, IoT integration depth, defrost engineering, and HACCP alignment — are interconnected. No single variable can be optimized in isolation. Procurement managers who approach the selection process with this systems-level perspective consistently achieve better ROI outcomes, fewer compliance incidents, and longer equipment service lives.
Frequently Asked Questions
Q: What is the difference between a blast freezer tunnel and a standard cold storage freezer?
A: A blast freezer tunnel uses high-velocity forced air — typically at 2–6 m/s — to rapidly freeze products on a moving conveyor, reducing core temperature to −18°C in minutes rather than hours. A standard cold storage freezer uses static or low-circulation air and freezes product over many hours, producing larger ice crystals and higher drip loss.
Q: How do I calculate the right freezing capacity (BTU) for my production volume?
A: Start with your target throughput in lbs/hour, multiply by the product's specific heat above and below freezing plus the latent heat of fusion (approximately 144 BTU/lb for water-based foods). Add 20–25% safety factor for fan heat load and infiltration. A refrigeration engineer should validate final sizing, especially for products with high moisture content or variable incoming temperatures.
Q: Is an IQF tunnel freezer worth the premium over a standard belt tunnel?
A: For particulate products — shrimp, diced vegetables, berry fruits — yes. IQF tunnels prevent clumping, improve individual piece quality, and command higher retail price points. For solid or formed products (burger patties, fish portions), a standard belt tunnel or plate freezer typically offers equal quality at lower capital cost.
Q: How often should defrost cycles run in a continuous blast freezer tunnel operation?
A: For typical U.S. food plant ambient conditions, hot-gas defrost every 8–12 hours is standard. High-moisture products may require defrost every 4–6 hours. Demand-initiated defrost controllers — triggered by evaporator pressure differential rather than a time clock — optimize cycle frequency and reduce unnecessary downtime by 15–25%.
Q: What refrigerant should I specify for a new blast freezer tunnel in 2026?
A: For large-scale operations (above 1,500 lbs/hour), ammonia (NH₃) or CO₂ transcritical systems are the strategically sound choices due to zero GWP, long-term regulatory stability under AIM Act phase-down schedules, and superior energy efficiency. For smaller commercial blast freezers, CO₂ subcritical or HFO-blend systems offer a compliant, lower-risk alternative with simpler facility requirements.
Keywords:
Inquiry
If you are interested in our products, please leave your email to receive a free product quote, thank you!
More information
Tel:
Sales E-mail: